Opening problem: safety gaps that start as small choices
Project teams often begin battery lines assuming mechanical design and PLC logic will cover safety; soon they find regulatory gaps, unexpected failure modes, and operator risk. When you start talking about battery manufacturing automation you must ask basic, practical safety questions right away — not later. A problem-driven approach forces the team to surface trade-offs early and keeps compliance work focused on real risks rather than checkbox exercises.
Which hazards are we actually trying to control?
List the concrete failure modes you might see on the line, with owners for each. Typical items to call out:- Thermal runaway risks during cell handling and formation.- Mechanical pinch and entrapment points on robotic cells.- Electrical arc or short during inspection and formation steps.- Software logic that permits unsafe states during maintenance.Give each hazard a simple severity and likelihood rating and attach an action owner. Those ratings show where to put engineering effort first rather than guessing.
Do our safety requirements map to recognised standards?
Cross-reference requirements with standards that matter to both automotive and batteries: ISO 26262 for vehicle-level functional safety and IEC 62133 for cell-level safety. Demonstrate how each control maps to a clause or risk statement. That traceability is proof for auditors and reduces rework when reviewers ask “show me where this came from”. My teams have relied on this mapping to keep reviews concise and defensible.

How will we verify safety under real operating conditions?
Verification must include simulated faults, stress tests, and human-in-the-loop checks. Build test scenarios that mimic operator errors, power interruptions, and cell variability. Use a combination of software-in-the-loop tests, hardware-in-the-loop runs, and at least one full-production pilot run to find interactions that bench tests miss. Where automation interfaces to manual tasks, test handover timing and fail-safe performance specifically.
What should we measure to know the line remains compliant?
Choose a short, objective set of indicators you will monitor daily:- Safety interlock trip frequency.- Near-miss reports and root-cause trends.- Downtime caused by safety-related faults.- Audit checklist pass rate.Make those metrics visible on the factory floor and review them weekly. If a metric drifts, you want an immediate action plan rather than a late audit surprise.
Who owns safety during change — design, commissioning, or ops?
Assign responsibilities before any design change. Put a named functional safety engineer on the critical path for design changes, require commissioning sign-off from safety, and keep operations accountable for procedural compliance. A clear RACI prevents the handoff ambiguity that causes the biggest delays and creates hidden risk.
Which technical controls work best for battery automation lines?
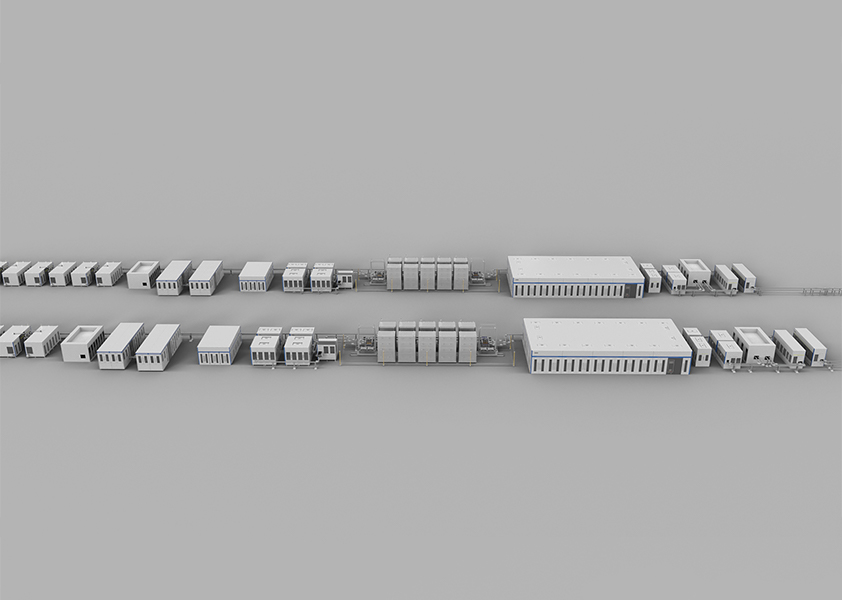
Choices should be guided by risk and by proven practices. Consider:- Hardware safety interlocks and safe torque off on robots.- Two-channel safety PLCs with diagnostics.- Redundant sensors on critical measurements like temperature and voltage.- Image analysis for detecting misfeeds or cell swelling.When evaluating system vendors, verify how they design for safe fallback states and automated isolation. Also compare architectures: centralised safety controllers versus distributed safe I/O — each has trade-offs in latency and maintainability. For teams choosing platforms, look at established integrators who already do automation for battery manufacturing and can show traceable verification artifacts.
Common pitfalls teams fall into
Avoid these repeated mistakes:- Designing safety as an add-on after production logic is frozen.- Over-relying on single-point sensors without diagnostics.- Treating human error as an excuse instead of designing to reduce it.- Waiting for the first incident to define safety work.Address these early and you’ll keep project timelines and costs predictable.
Practical commissioning checklist
Before handover, complete these steps:- Functional safety validation with recorded test logs.- Operator task training and signed competency checks.- Maintenance mode procedures and lockout/tagout verification.- Emergency stop and safe-state timing tests.Keep the evidence in one place so external audits or customer reviews can be completed quickly.
Experience and a single real-world anchor
Teams in major battery production hubs, notably Guangdong province in China, have shown how small design choices scale into program-level risks. Decades of work in automation and safety engineering teach that early mapping to standards, repeated verification under production conditions, and clear ownership prevent surprises during scale-up. That practical experience is what makes compliance actionable instead of theoretical.
Final synthesis — what a project team gains
A problem-driven lens keeps teams honest: identify hazards, map to standards, verify against real conditions, and assign ownership. When those elements are in place, designs remain auditable and operators stay safe. The result is a clear, defendable approach that aligns engineering choices with production realities and the consultancy support that helps make it tangible, as provided by FHS.